China United Mould

Logo 2021
CNC turning

CNC turning and Swiss-type turning for round parts

In CNC turning the bar or blank rotates and a stationary tool cuts it. For round parts such as shafts, pins, bushings, spacers, fittings and threaded parts, turning is usually faster than milling, and diameters turned in one clamping stay concentric. In Swiss-type turning a guide bushing supports the bar right next to the tool, so long, slender, small-diameter parts stay straight while they are cut.

Turned parts can also carry flats, cross holes and slots, and can go on to grinding, plating or heat treatment.

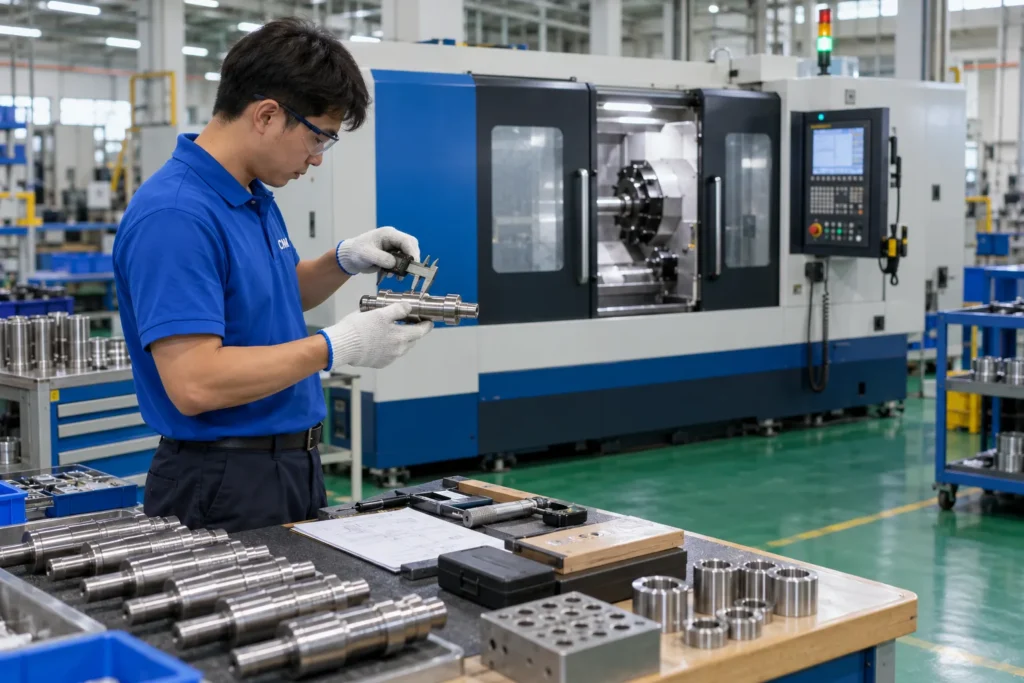
Operator checking a turned stainless steel shaft with a caliper next to a CNC lathe
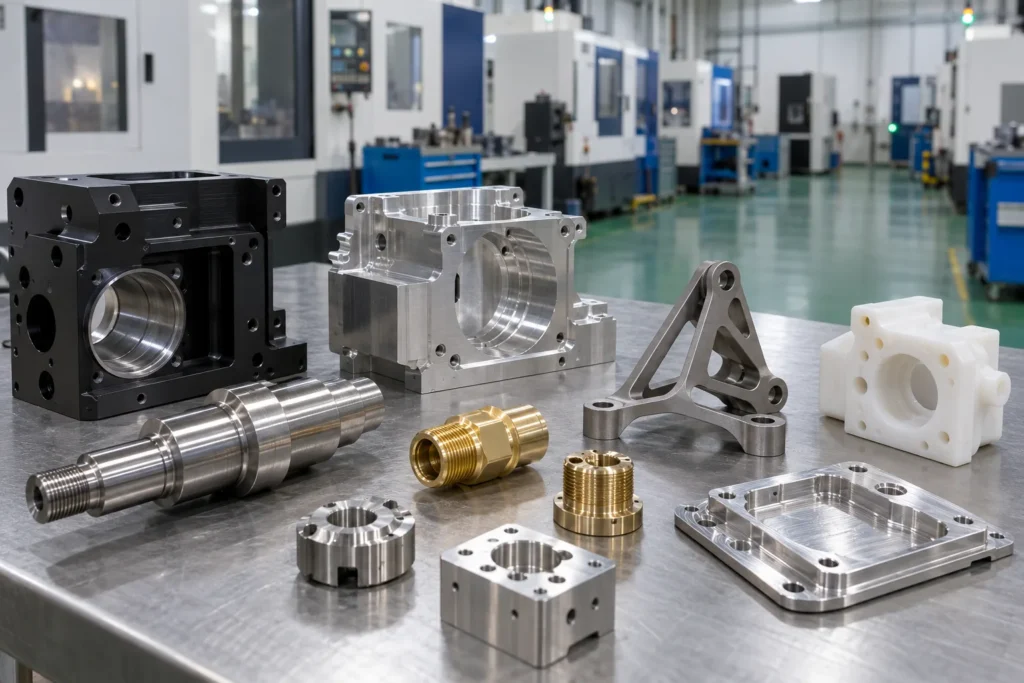
CNC machined aluminum housings, steel shafts, brass fittings and a POM part

Typical turned parts

CNC turning at a glance (typical)

ProcessesCNC turning and Swiss-type turning; flats, slots and cross holes milled as a second operation where needed
Typical partsShafts, pins, bushings, spacers, fittings, threaded parts
FeaturesDiameters, faces, tapers, grooves, threads, knurls
Surface roughnessRa 1.6–3.2 µm as turned; Ra 0.4–0.8 µm by grinding
MaterialsAluminum, free-machining and stainless steels, brass, copper, titanium, plastics
SecondaryGrinding, thread rolling, heat treatment, plating

CNC turning FAQ

What is Swiss-type turning?

A turning method where the bar slides through a guide bushing right next to the cutting tool. The support keeps long, slender, small-diameter parts straight while they are cut, which suits small precision parts made from bar in volume.

Can turned parts have milled features?

Yes. Flats, slots, cross holes and off-center holes are made on lathes with driven tools or in a separate milling operation. The route depends on the part and the quantity.
Have a drawing ready? Send it for a quotation.